
Direct Factory Sourcing for Precision Fittings Carbon Steel Components
Sourcing reliable, precision-engineered carbon steel pipe fittings directly from an ISO-certified CNC machining manufacturer eliminates premature fatigue failures, pressure-line bursts, and expensive assembly downtime. As a specialized OEM/ODM manufacturer of custom carbon steel fittings, we produce high-integrity fluid power adapters, forged hydraulic connectors, SAE split flanges, and integrated valve blocks built strictly to custom engineering specifications.
Equipped with 80+ high-precision CNC turning centers, automated gantry robotics, and 4-axis machining centers, our facility supports procurement teams from 7-day rapid prototyping to automated high-volume production. Whether your project demands cross-standard thread conversions, quenched and tempered structural blanks, or automotive-grade anti-corrosion finishes, our engineering team guarantees tight dimensional tolerances down to ±0.02 mm and zero-leakage sealing across demanding carbon steel pipe and fittings applications.
Solved Engineering Challenges in Industrial Fluid and Hydraulic Systems
High-pressure fluid lines, heavy machinery, and aggressive operating environments present serious mechanical hurdles. Standard commercial carbon steel fittings often fail under severe pressure surges, continuous cyclic vibration, and atmospheric corrosion.
Fatigue Failure and High-Pressure Dynamic Surges
Standard low-carbon components frequently lack the core toughness required to endure continuous pressure pulses. We utilize targeted quenching and tempering (Q&T) on medium-carbon and alloy steels (AISI 1045, 4140) to transform the internal matrix into a refined tempered sorbite structure, boosting yield strength and fatigue limits under high-pressure hydraulic cycles.
Accelerated Oxidation and Environmental Corrosion
Unprotected carbon steel oxidizes rapidly in humid and coastal conditions. Our factory delivers an expansive range of engineered electroplating and conversion coatings, including automotive-grade zinc-nickel alloy plating certified to resist red rust for 1,000+ hours in ASTM B117 neutral salt spray testing.
Mismatched Global Thread Standards and Thread Galling
Cross-standard thread transitions—such as NPT/NPTF to BSPP, SAE ORB (O-Ring Boss) to Metric heavy series (DIN 2353), or JIC 37° flare—frequently suffer from pitch runout or galling during makeup. We turn and chase all thread profiles in-house with PVD nano-coated tooling, controlling pitch diameters and lead consistency to prevent thread seizure.
Concentricity Deviation and Fixture Jaw Damage
Multi-setup operations across discrete lathes introduce concentricity errors and leave clamping indentations on critical sealing surfaces. Our automated CNC turning centers utilize dual-spindle synchronized pickups, soft pie jaws, and internal expanding mandrels to achieve 0.01 mm to 0.02 mm concentricity with zero surface damage.
Manufacturing Scope: Custom Carbon Steel Pipe and Fittings
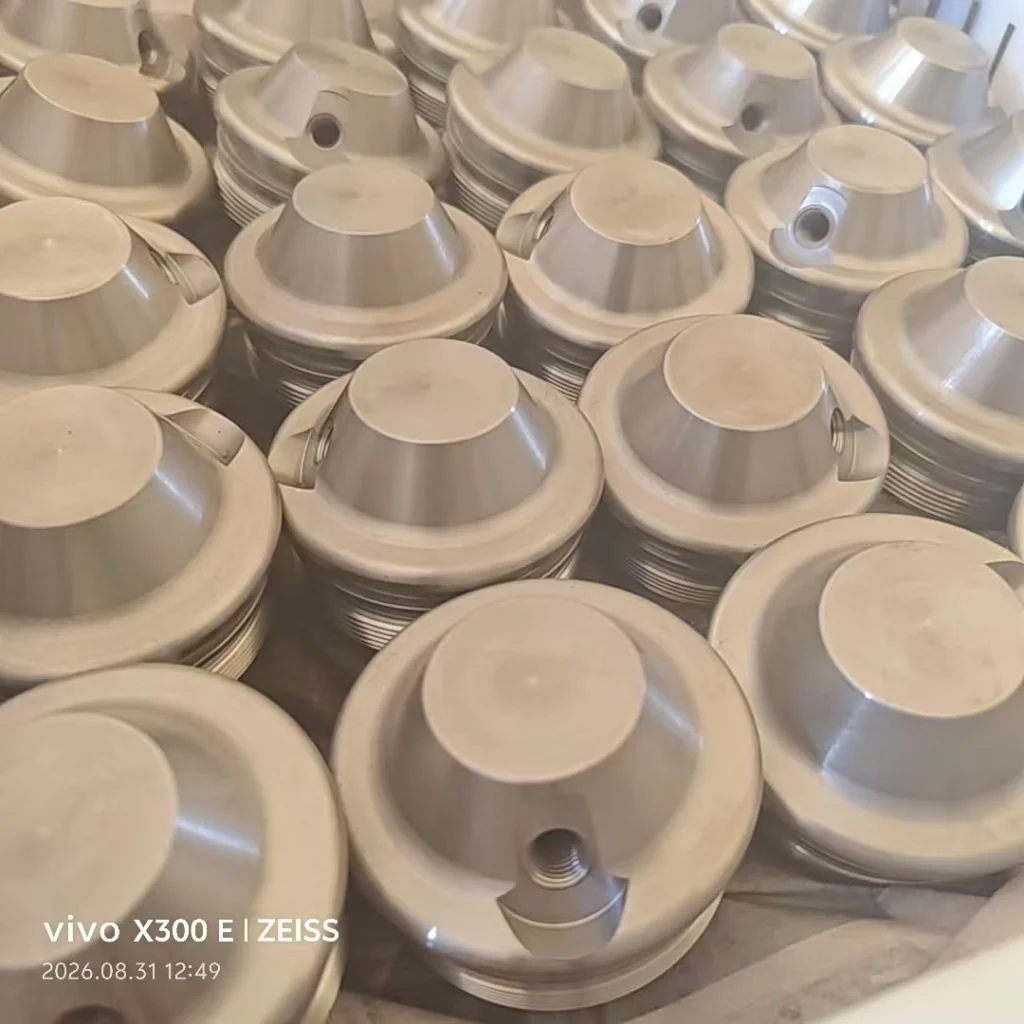
Our multi-axis CNC cells process cold-drawn hex and round bar stock, heavy-wall seamless mechanical tubing, hot-forged blanks, and precision cold-headed preforms into a complete line of high-pressure fluid power components.
Hydraulic Thread Adapters and Hex Fittings
High-speed CNC-turned straight adapters, bulkhead connectors, expanding bushings, and hex nipples with NPT, NPTF, BSPP, BSPT, Metric, and UNF/UN thread profiles featuring precision-machined O-ring and elastomeric retaining grooves.
Machined High-Pressure Elbows, Tees, and Crosses
Produced from dense hot forgings or solid square/hex bar stock to completely eliminate the internal shrinkage cavities, micro-porosity, and flow-line defects common in cast fittings carbon steel under surge pressures up to 10,000 PSI (700 bar).
SAE 4-Bolt Flanges and Split Flange Halves
Face-turned and multi-spindle drilled Code 61 (3,000 PSI) and Code 62 (6,000 PSI) standard and companion flanges delivering smooth sealing faces (Ra ≤ 1.6 μm) for leak-free, heavy-duty pipe connections.
Multi-Port Manifold Blocks and Valve Enclosures
Manufactured on 4-axis horizontal and vertical machining centers, featuring complex internal deep-hole cross-drilling, cavity porting, and strict geometric flatness tolerances (≤ 0.03 mm) for hydraulic distribution assemblies.
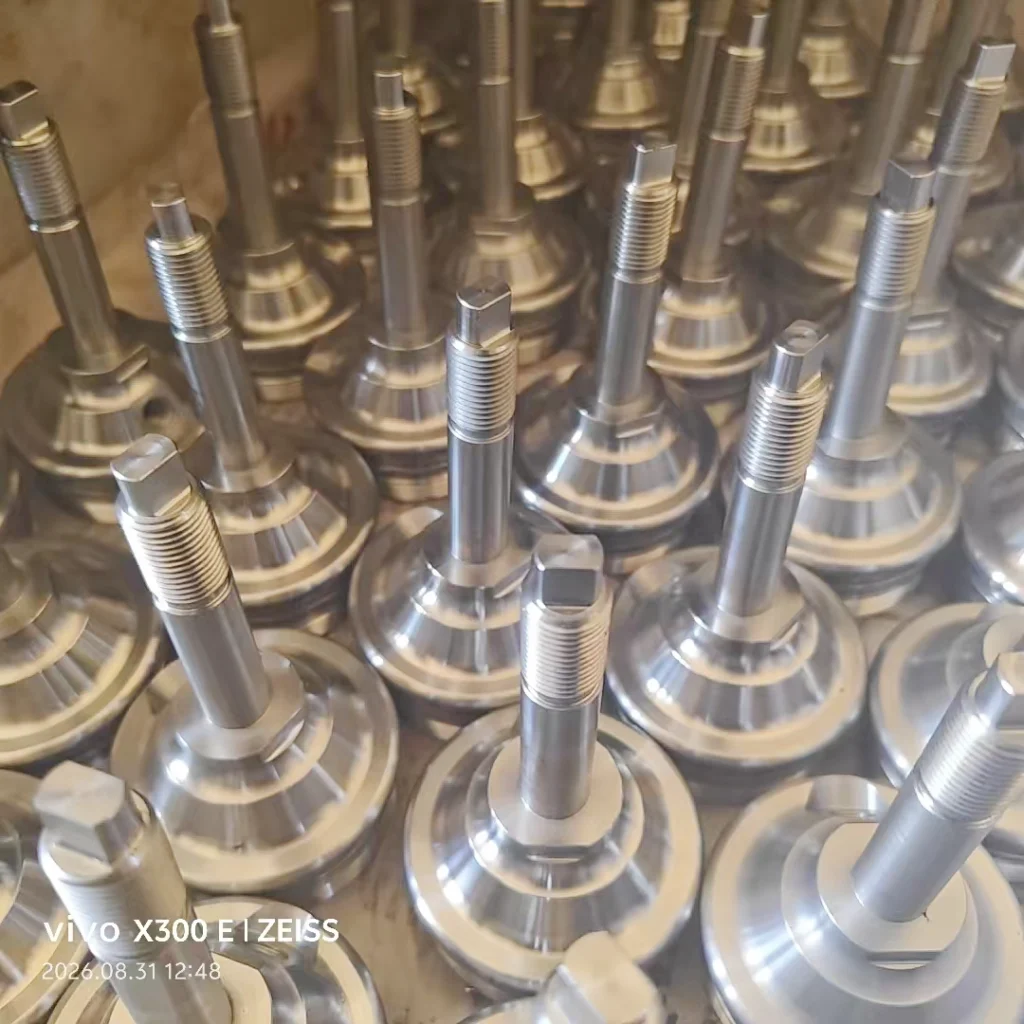
Carbon Steel Material Spectrum and International Grade Cross-Reference
Matching the correct steel grade to your structural and environmental requirements ensures the right balance of machinability, core hardness, tensile strength, and cost-efficiency across all carbon steel pipe fittings.
| Material Category | USA (ASTM / AISI) | China (GB/T) | Japan (JIS) | Europe (EN / DIN) | Machinability & Mechanical Properties | Best Use Cases in Carbon Steel Fittings |
| Free-Cutting Steel | 1215 / 12L14 | Y15 / Y15Pb | SUM22 / SUM24L | 11SMn30 / 11SMnPb30 | Exceptional chip breaking, high-speed turning, and smooth surface finish; non-weldable. | High-volume straight adapters, hex nipples, port plugs, and non-welded connectors. |
| Low Carbon Steel (Weldable) | 1020 / A105 | 20# / Q235B | S20C / SS400 | C22E / 1.0402 | High elongation and ductility; ideal for cold bending, forming, and structural welding. | Welded hydraulic tube ends, split flanges, low-pressure plumbing sockets, and forged bodies. |
| Medium Carbon Steel (Q&T) | 1045 / UNS G10450 | 45# | S45C | C45E / 1.1191 | High tensile strength and fatigue resistance after quenching and tempering; balanced machinability. | Heavy-duty hydraulic adapters, high-pressure union nuts, forged elbow bodies, and valve stems. |
| Cr-Mo Alloy Steel | 4140 / UNS G41400 | 42CrMo | SCM440 | 42CrMo4 / 1.7225 | Superior hardenability, high yield strength, and impact toughness under extreme shock loads. | Ultra-high-pressure hydraulic manifolds (700+ bar), offshore flange couplings, and critical fluid blocks. |
| Low-Temp Carbon Steel | A350 LF2 | 16Mn / Q345D | S35C | 1.0566 / TStE355 | Retains impact toughness down to -46°C; fine grain structure with strong yield characteristics. | Low-temperature oil & gas piping systems, refrigeration hydraulic blocks, and subsea connectors. |
Thermal Processing and Quenching & Tempering (Q&T) Workflow
For critical high-pressure and dynamic shock applications, controlling internal grain structure through heat treatment is vital:
[Raw Bar / Forging Blank] ➔ [Rough CNC Turning] ➔ [Quenching & High-Temp Tempering] ➔ [Finish CNC Machining & Thread Chasing] ➔ [Surface Treatment & Plating]
Quenching and High-Temperature Tempering (Q&T)
Medium-carbon steel (AISI 1045) and chromium-molybdenum alloy steel (AISI 4140) are austenitized at 840°C to 860°C, rapidly quenched in agitated oil or polymer solutions, and tempered at 550°C to 650°C. This process achieves:
-
Tempered sorbite microstructure providing optimal toughness.
-
Yield strength: ≥ 550 to 750 MPa.
-
Core hardness: HBW 220 to 280 (HRC 22 to 30).
-
Minimum elongation: ≥ 15% for dynamic impact resistance.
Localized Surface Induction Hardening
Applied to internal valve seats, sealing tapers, and critical wear interfaces to achieve HRC 48 to 55 surface hardness while preserving a ductile, shock-absorbing core.
Sub-Critical Stress-Relief Annealing
Conducted at 580°C to 620°C following rough machining or cold extrusion to relieve residual stresses and prevent dimensional distortion during finish grinding and thread chasing.
Engineered Surface Finishing Solutions for Carbon Steel
Because raw fittings carbon steel grades are prone to oxidation, we provide comprehensive surface finishing solutions to meet rigorous environmental and mechanical standards:
| Surface Treatment | Coating Thickness | Neutral Salt Spray (ASTM B117) | Appearance / Visual Finish | Key Characteristics & Ideal Applications |
| Trivalent Blue/White Zinc (Cr3+) | 3–15 μm | 24–120h White Rust / 240h Red Rust | Bright Silver / Clear Blue | Cost-effective, RoHS/REACH compliant. Standard finish for general indoor hydraulic systems and mobile equipment. |
| Trivalent Yellow / Rainbow Zinc | 3–15 μm | 24–168h White Rust / 360h Red Rust | Iridescent Rainbow Yellow | Thicker chromate film providing enhanced barrier protection for agricultural machinery and outdoor fluid lines. |
| Zinc-Nickel Alloy Plating (Zn-Ni) | 5–12 μm (12–15% Ni) | 1,000+ Hours Red Rust | Uniform Silver-Grey or Black | Automotive and marine benchmark; exceptional corrosion resistance, high thermal tolerance (up to 200°C), and low galvanic potential. |
| Electroless Nickel Plating (ENP) | 10–25 μm (Mid/High-P) | 500–1,000+ Hours Red Rust | Semi-Bright Metallic Grey | 100% uniform deposit thickness across internal cross-holes and blind threads. High hardness (45–50 HRC as-plated), superior wear and chemical resistance. |
| Hard Chrome Plating | 15–50 μm | 200–500 Hours Red Rust | Mirror / Bright Metallic | Extreme surface hardness (65–70 HRC), low coefficient of friction. Best for sliding valve spools, hydraulic piston rods, and abrasive slurry lines. |
| Electroplated Gold | 0.5–2.5 μm (over Ni sub-layer) | 96–240 Hours Red Rust | Lustrous Golden Yellow | Outstanding electrical conductivity, zero contact oxidation, and chemical inertness. Used in specialized sensor test ports and aerospace fluid instrumentation. |
| Manganese / Zinc Phosphating | 3–8 μm (+ Oil Seal) | 24–48 Hours (Oil-Retained) | Matte Dark Grey / Black | Excellent oil retention, friction reduction, and anti-galling properties; ideal for threaded unions and break-in wear protection. |
| Black Oxide | 1–2 μm (+ Rust Inhibitor Oil) | 24–72 Hours | Glossy Deep Black | Zero dimensional buildup (sub-micron conversion layer); suited for high-precision indoor fittings, optical instruments, and precision fixture parts. |
Dimensional Allowance for Plating Buildup
To prevent thread binding on class 6g/6H and 2A/2B fits, our CNC programming offsets pitch diameters prior to plating, accounting for coating buildup (e.g., 8–15 μm zinc or ENP layers) and ensuring 100% Go/No-Go thread gauge compliance post-treatment.
Quality Assurance Protocols and Process Flow
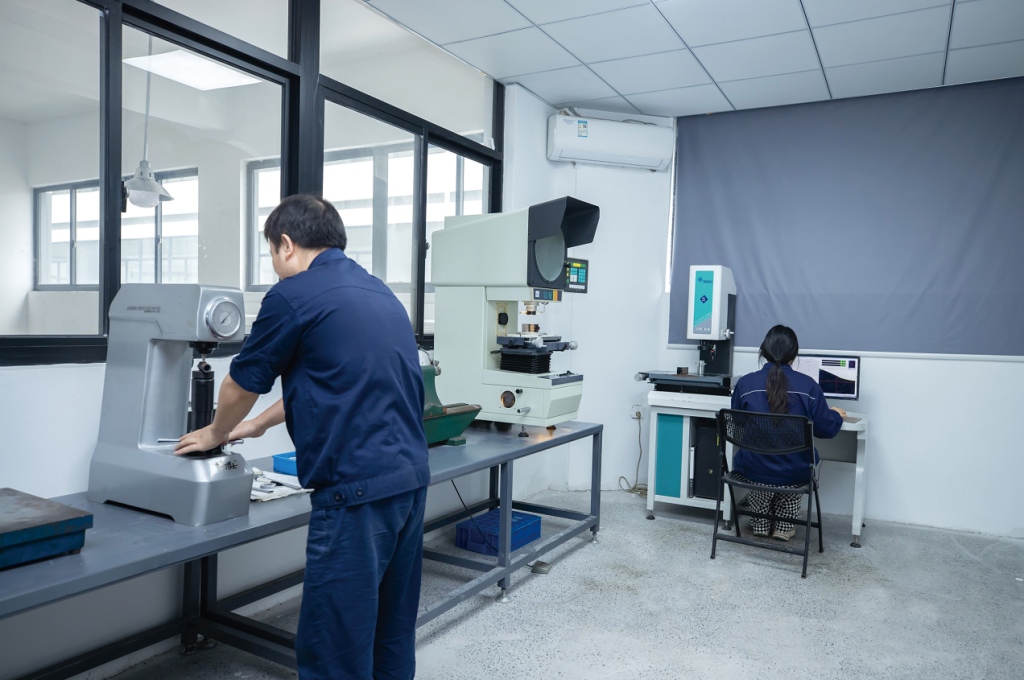
Every production run at our factory follows rigid quality validation checkpoints:
Optical Emission Spectrometry (OES) Verification
Every raw bar, casting, and forging lot is spectrographically tested to verify Carbon (C), Manganese (Mn), Chromium (Cr), and Molybdenum (Mo) elemental composition against EN 10204 3.1 standards.
In-Process Thread and Sealing Inspection
100% of turned threads are verified using calibrated Go/No-Go thread gauges, optical profile projectors (2.5D), and contact contour measuring systems to evaluate 37°/24°/60° sealing taper angles and surface roughness (Ra ≤ 0.8 μm).
Plating Thickness and Salt Spray Auditing
Coating layers are measured with X-Ray Fluorescence (XRF) and magnetic induction gauges. In-house cyclic salt spray testing cabinets validate batch corrosion performance against ASTM B117 standards.
Ultrasonic Cleaning and Anti-Corrosion Packaging
Machined parts undergo multi-stage ultrasonic degreasing, clean-air drying, and protective oil dipping before being individually sealed in heavy-gauge poly bags to prevent moisture contact and thread impact damage during ocean transport.
[2D/3D CAD Drawing / RFQ] ➔ [DFM Review & Tooling Plan] ➔ [7-Day Prototyping & Heat Treatment] ➔ [Automated CNC Production] ➔ [Plating & Surface Coating] ➔ [100% Inspection & MTC Certification] ➔ [Export Packaging & Global Delivery]
Frequently Asked Questions (FAQ)
What material test certificates and inspection reports are supplied with each batch?
We provide full EN 10204 3.1 Mill Test Certificates (MTC) covering raw material melt chemistry, mechanical tensile and yield data, heat treatment batch hardness charts, plating thickness reports, and full-dimensional CMM inspection logs.
How do you prevent thread galling, binding, and micro-burrs on custom carbon steel fittings?
We implement precision thread-milling and single-point turning using PVD-coated carbide inserts with dedicated chip-breakers. All components undergo secondary vibratory tumbling or thermal deburring to eliminate micro-burrs before surface plating.
Can your facility meet strict automotive OEM zinc-nickel plating specifications?
Yes. Our zinc-nickel plating lines deliver an engineered 12% to 15% nickel content adhering to ISO 19598 and ASTM B841 specifications, regularly verified to exceed 1,000 hours of neutral salt spray testing without red rust formation.
Partner with a Direct Factory for Custom Carbon Steel Pipe Fittings
Eliminate supplier markups, shorten manufacturing lead times, and secure fully certified carbon steel pipe fittings engineered strictly to your blueprints. Contact our technical team today to submit your RFQ and receive a comprehensive Design for Manufacturability (DFM) review along with a factory-direct quote within 24 hours.


