
Why Standard Pipe Components Fall Short in High-Pressure Systems
-
Envelope and Port Constraints: Off-the-shelf adapters often feature bulky hex profiles or standard lengths that interfere with adjacent ports on compact manifold blocks, pump housings, or skid assemblies.
-
Complex Multi-Joint Assemblies: Linking disparate ports often requires chaining together an elbow, a nipple, and a reducing bushing. Every extra threaded interface introduces an additional potential leak path under dynamic vibration.
-
Corrosion Mismatches: Commercial fittings frequently utilize generic stainless alloys without certified traceability, leading to localized pitting in chloride-heavy or marine environments.
4 Essential Engineering Dimensions for Application-Specific NPT Fittings
1. Geometry and Spatial Envelope
-
Integral Step Reductions: Transitioning from large nominal pipe sizes down to miniature ports without multi-piece stacking.
-
Low-Profile and Extended Lengths: Tailored hex flats, ultra-short threaded shanks for confined clearances, or extended bulkhead fittings for passing through heavy equipment panels.
-
Monolithic Multi-Port Bodies: Complex 90° elbows, tees, and cross adapters CNC machined directly from solid billet blocks to maximize burst pressure resistance.
2. Alloy Selection and Severe-Service Integrity
-
Material Grades: Selection spans austenitic alloys (SS304/304L, SS316/316L, 316Ti) for general chemical resistance, heat-stabilized grades (SS321, SS310S) for thermal cycling, and Duplex alloys (2205, Super Duplex 2507) for high-pressure sour gas and offshore desalination.
-
Calculated Wall Thickness: Hex body sizing and internal core diameters are proportioned to support operating pressures from 3,000 PSI up to 15,000 PSI with safety factors of 4:1.
3. Hybrid and Cross-Standard Thread Configurations
-
Male NPT to Female BSPP (with integral O-ring undercut or flat face bonded seal).
-
Male NPTF to Metric ISO 6149 / ISO 261 port adapters.
-
Female NPT to JIC 37° flare or ORFS (O-Ring Face Seal) hydraulic interfaces.
4. Specialized Surface Treatments
-
Ultrasonic Degreasing: Multi-stage cleaning to remove hydrocarbon residues for oxygen-clean or semiconductor fluid service.
-
Chemical Passivation (ASTM A967): Removing free iron from machined surfaces to maximize chromium-oxide corrosion resistance.
-
Electropolishing: Achieving an ultra-smooth finish (Ra ≤ 0.4 μm) inside internal flow bores to eliminate flow turbulence and particle entrapment.
Technical Deep-Dive: NPT vs. NPTF Sealing Mechanisms and Tooling Demands
What Is an NPT Thread? (ANSI/ASME B1.20.1)
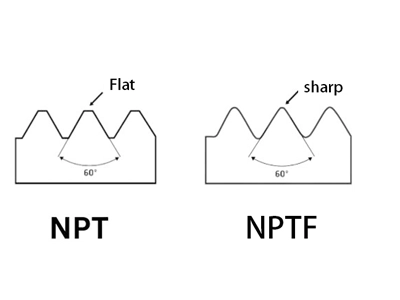
An NPT (National Pipe Taper) thread is the standard North American tapered pipe thread defined by ANSI/ASME B1.20.1, featuring a 60° thread angle and a 1:16 taper ratio (3/4″ taper per foot). When standard NPT fittings are torqued into a mating port, mechanical holding strength is achieved along the thread flanks.
However, because standard NPT geometry leaves a microscopic clearance between the thread crests and roots, fluid or gas can track along this spiral path under pressure. Therefore, standard npt pipe fittings strictly require a quality thread sealant—such as PTFE tape or anaerobic paste—to fill the root clearance and establish a dependable, leak-free seal in general industrial piping.
What Is an NPTF Thread? (Dryseal – ANSI B1.20.3)
An NPTF (National Pipe Taper Fuel / Dryseal) thread is an engineered high-performance variant governed by ANSI B1.20.3, purpose-built for applications where liquid sealants cannot be used. While it shares the same 60° thread angle and 1:16 taper as standard NPT, the root and crest truncations are machined to much tighter dimensional tolerances.
During assembly, the sharp crests of the NPTF thread mechanically crush and plastically deform into the mating roots before flank contact occurs. This deliberate interference creates a true 100% metal-to-metal pressure-tight seal without thread tape or paste. NPTF npt fittings are the industry standard in critical fluid circuits where sealant debris could clog downstream valves, such as high-pressure hydraulic lines, fuel systems, and severe thermal cycling environments.
NPT (ANSI/ASME B1.20.1): Standard Tapered Pipe Thread
-
Thread Geometry: 60° thread angle with a 1:16 taper ratio (3/4″ taper per foot).
-
Sealing Mechanics: Standard NPT threads feature clearance between the crests and roots during assembly. Flank-to-flank contact provides mechanical hold, but fluid will track along the spiral clearance path unless filled with a high-performance PTFE tape or anaerobic paste sealant.
NPTF (ANSI B1.20.3): Dryseal Taper Pipe Thread
-
Thread Geometry: 60° thread angle with a 1:16 taper ratio, but with strictly controlled truncation at both crest and root.
-
Sealing Mechanics: When tightened, the sharp crests mechanically crush into the mating roots before flank interference occurs. This forms a true 100% metal-to-metal seal without the use of thread tape or paste—crucial for high-temperature exhaust, fuel injection, and contamination-sensitive hydraulic circuits.
Thread Machining and Inspection Comparison
| Thread Standard | Thread Angle & Taper | Sealing Method | CNC Tooling & Inspection Requirements |
| NPT | 60° / 1:16 Taper | Thread flank contact + PTFE Tape/Paste | Single-point CNC threading or precision tapping; Verified via standard L1 taper plug/ring gauges. |
| NPTF (Dryseal) | 60° / 1:16 Taper | Metal-to-metal plastic crest/root crush | High-precision single-point CNC turning mandatory; Sharp crests accelerate insert tip wear; Verified with 3-gauge sets (L1, L2/L3, Crest/Root truncation gauge). |
| BSPT (ISO 7-1) | 55° / 1:16 Taper | Thread flank contact + Sealant | Radius crests/roots; Strict 55° tooling; Incompatible with 60° NPT ports. |
| BSPP (ISO 228-1) | 55° / Parallel (No Taper) | Elastomeric O-ring or flat washer | CNC turning with dedicated O-ring retention grooves and smooth sealing faces (Ra ≤ 0.8 μm). |
Precision CNC Machining and Quality Assurance Protocols
Eliminating Thread Galling (Cold Welding)
-
Controlled CNC cutting feeds produce clean, smooth thread flanks without micro-tears (Ra 0.8 – 1.6 μm).
-
Optimized chamfers and full deburring eliminate microscopic ragged edges that initiate metal pickup.
-
Complete nitric or citric acid passivation restores a uniform oxide layer before shipping.
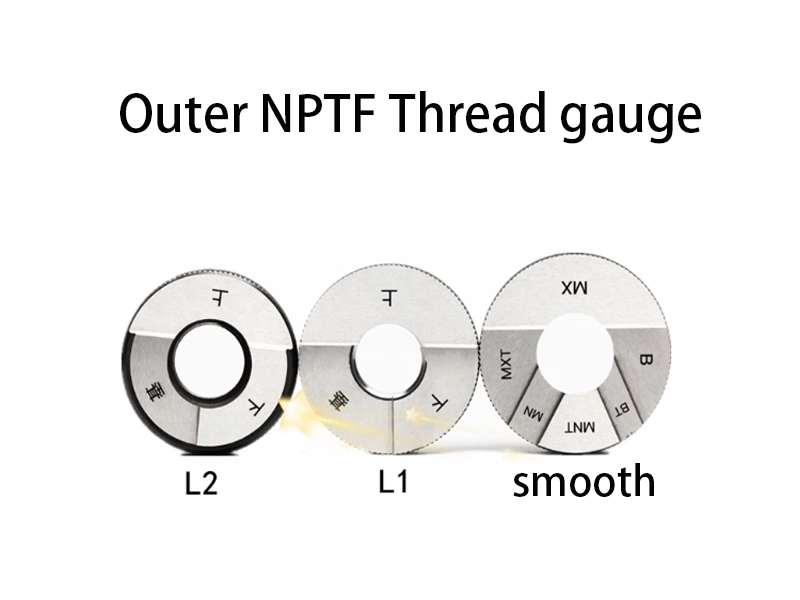
Rigid 3-Step Gauging for NPTF Dryseal Profiles
-
L1 Plug / Ring Gauge: Checks pitch diameter at the hand-tight engagement plane.
-
L2 / L3 Gauge: Verifies thread taper and effective pitch diameter through wrench-tight depth.
-
6-Step Crest/Root Gauge: Verifies that truncation dimensions sit precisely inside the allowable tolerance band.
Edge and Thread Protection During Global Transit
-
Individual Thread Caps: Every external male thread is fitted with a heavy-duty plastic protective sleeve immediately upon coming off the CNC lathe.
-
Individual Poly Bagging: Components are bagged individually or packed in partitioned grid cartons to prevent metal-on-metal contact during air or ocean transit.
Engineering Collaboration Workflow: From Drawing to Production
[2D / 3D Drawings (PDF/STEP)]
             │
             ▼
[DFM Review & 24h Quotation]
             │
             ▼
[Prototype Verification & CMM Report]
             │
             ▼
[Automated CNC Production & 100% Gauge Inspection]
             │
             ▼
[Ultrasonic Cleaning, Capped Packaging & Global Export]


